Bulk Rubber Profiles Extrusion Line for Consistent High-Volume Profile Manufacturing
2026-11-16
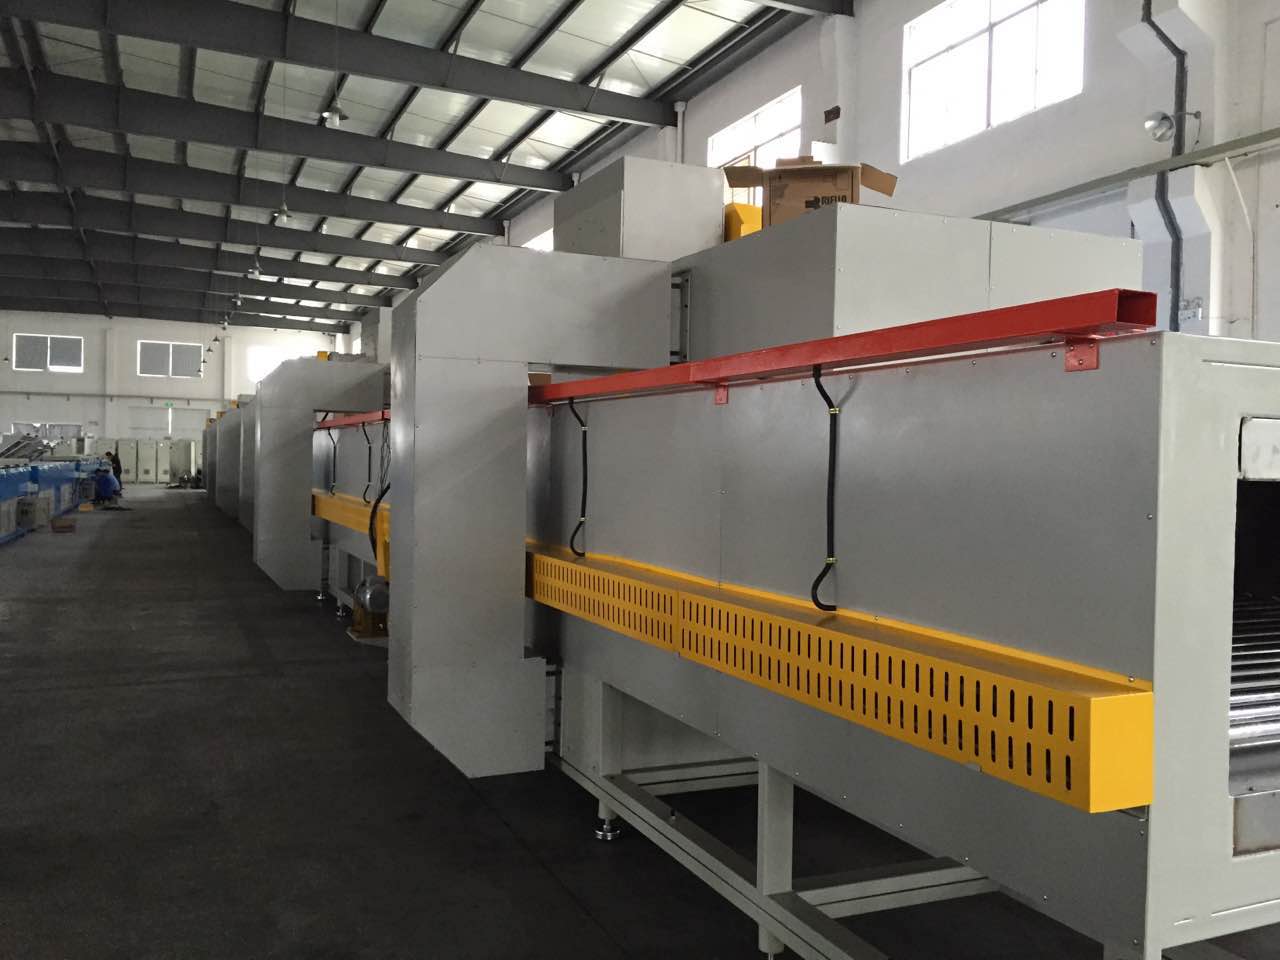
When your production schedule demands thousands of meters of uniform rubber profiles every week, the last thing you need is a line that hesitates. That’s where the bulk rubber profiles extrusion line steps in—purpose-built for high-volume consistency without the usual bottlenecks. At SFC, we’ve seen how the right extrusion setup can turn a chaotic production floor into a predictable, profit-driving operation. But what actually separates a true bulk line from a standard extruder? Let’s pull back the curtain on the engineering, material handling, and control systems that make consistent, high-output profile manufacturing possible.
Bulk Feed Systems That Don't Starve the Screw
Screw feeders often run into trouble when the hopper above them lets material bridge or form a rat hole. The screw ends up spinning in an air pocket while the rest of the bin holds back. To keep a bulk feed system from starving the screw, the entire cross-section above the inlet has to move downward at roughly the same rate. That means no stagnant corners, no sudden collapses, and no reliance on luck.
Mass flow hoppers help a lot here. Their walls are steep enough and smooth enough that every particle slides toward the discharge, so the screw sees a consistent bulk density from the first turn to the last. Funnel flow hoppers, by contrast, let material empty from the top center while the sides just sit there—until they break loose unpredictably. That kind of erratic feeding shows up as under-dosing, over-dosing, or a screw that runs dry for seconds at a time.
For sticky or fibrous materials, a well-designed hopper alone may not be enough. Mechanical agitators, vibratory discharges, or air pads near the outlet can keep the material active without packing it tighter. It also pays to match the screw to the job: variable pitch or a tapered shaft can draw material evenly along the inlet opening instead of pulling mostly from the back. When the bin, the flow aid, and the screw are designed as one system, the screw is far less likely to starve.
Why Die Pressure Fluctuations Show Up as Thin Walls
In die casting, the filling phase depends on a steady pressure profile to push molten metal into every cavity detail. When that pressure oscillates, the metal front can stall or surge at unpredictable moments. Regions that depend on sustained pressure to remain fluid until the cavity is fully packed may instead start to solidify early. The result is a section that never receives the full intended metal volume, leaving behind a wall thinner than the tool design specifies.
These fluctuations often trace back to the shot end rather than the die itself. A worn plunger tip, inconsistent hydraulic accumulator pressure, or a sluggish valve can cause the injection force to vary by several bar within milliseconds. Because the metal is already losing heat as it travels through the runner, any momentary drop in pressure means less force to overcome viscous resistance and keep the metal moving into thin features. The cavity wall then freezes before the pressure recovers enough to pack more material, locking in the thin-wall defect.
Adjusting Line Speed Without Sacrificing Profile Tolerance
Raising line speed often feels like a direct trade-off against profile tolerance, but that mindset overlooks how modern motion control handles acceleration and deceleration. Instead of pushing a constant high velocity through every feature, break the toolpath into segments where speed is reduced only at sharp radii or tight corners. This lets the machine hold tight profile bands on critical geometry while still covering long straight sections at full throughput.
The practical approach combines jerk-limited cornering with look-ahead feed control. When the controller knows a tight radius is coming, it can ease into the turn without overshooting the contour. Pair this with a slight increase in feed on open, low-curvature regions, and the overall cycle time improves without any measurable drift in profile deviation. Some shops also fine-tune servo gains or use dynamic fixture offsetting to counter the small inertial effects that show up only at higher traverse rates.
Validation matters more than guesswork here. Run a short test coupon with a known profile tolerance, then compare CMM or laser scan data before and after adjusting the speed map. In most cases, a carefully tuned variable-speed program will match or beat the profile results of a slower, uniform feed — while cutting significant time off the job.
Cooling Troughs Designed for Heavy, Thick Sections
Heavy, thick sections don't cool like thin plate or bar stock. The thermal mass resists rapid temperature changes, and if you push too hard, you get steep gradients between the surface and the core. That's exactly where ordinary troughs fail—they can't move enough fluid or maintain a controlled quench across the entire cross-section, so distortion and residual stress become the norm. A properly engineered cooling trough for these sections isn't just a bigger tank; it's built around the physics of delayed heat rejection.
These troughs typically feature reinforced sidewalls and baffled inlet zones to handle the volume and velocity needed for high-capacity cooling. Agitation is tuned rather than brute-force, because a violent quench on a thick forging can crack it before the center even notices the temperature drop. Many designs incorporate variable-speed circulators or adjustable weir plates, letting you shift the cooling rate depending on wall thickness and alloy. The result is a more uniform drop through the section, which matters when you're chasing tight dimensional tolerances or looking to avoid post-quench straightening.
What separates a good heavy-section trough from a repurposed standard one is what happens after the first few seconds. Surface temperature falls fast, but the core still holds a lot of heat, so the cooling medium must keep working against a shifting gradient. Some troughs add a secondary low-flow zone or a directional return line that keeps fresh quenchant sweeping the same faces without creating a stagnant hot layer. It's a practical, working solution for thick plate, die blocks, and large castings where uneven cooling isn't just an inconvenience—it's a scrap generator.
Inline Cutting Without Deforming Soft Rubber
Soft rubber’s low modulus and high elasticity make it want to squirm away from any blade. To cut inline without distortion, the material path must be stabilized right at the cut zone. A close-fitting guide or vacuum belt holds the profile in place instead of relying on the rubber’s own stiffness, so the blade sees a consistent cross-section. That removes the chance of local buckling or stretching before the edge even makes contact.
Blade geometry and speed matter just as much as support. A hollow-ground or ultrasonically oscillating blade reduces downward force enough to avoid compressing the surface, while a fast single-pass motion prevents the rubber from heating and sticking. For thicker sections, a slight counter-rotation or a low-friction coating on the blade flanks lets the cut faces separate cleanly. Inline cutting then holds tolerances tight without a secondary trimming step.
Data Logging for Repeatable Batch-to-Batch Output
Batch processes rarely fail all at once. They drift. A temperature probe reads a degree low for an afternoon, a mixer slows by two RPM, an operator shortens a purge cycle to make up time on a Friday shift. None of these events shuts down a line, but together they shift the output just enough that the next batch no longer matches the last. Data logging is what turns those quiet drifts into visible pattern breaks. Without a continuous record, the only signal you get is a rejected lot and a scramble to guess what changed.
The log needs to capture more than final readings. Record the setpoint and the actual value, the ramp rate, the hold time at each stage, ambient conditions, raw material lot numbers, and even which operator ran the line. Sampling every ten seconds is often enough for slow thermal processes, while faster mixing or reaction steps may need sub-second capture. Store the raw timestamps, not just averages. Averages hide the five-minute excursion that ruined a viscosity curve. Keep the data in a queryable format, not locked inside a PDF report that no one can search later.
The point of all this is repeatability, not just traceability. When a batch meets every spec, pull its log and use it as the reference fingerprint. Compare each new run against that fingerprint as it progresses, not after the fact. A simple overlay of current temperature trace versus the last three good batches will show a divergence long before it becomes a defect. Set thresholds on deviation rate, not just absolute limits. If the trend line for pressure starts bending away from the reference by more than a fraction per minute, alert the operator while there is still time to correct. Over months, these reference fingerprints become the real recipe, more reliable than any written procedure.
FAQ
It handles solid, sponge, and co-extruded profiles with cross-sections ranging from simple strips and tubing to complex multi-hollow seals. Common outputs include door seals, window gaskets, edge trims, and industrial bumper profiles.
Closed-loop control on barrel temperatures, screw speed, and haul-off tension keeps the extrudate stable. A laser or optical gauge checks key dimensions inline, and automatic adjustments to puller speed correct minor drift before it becomes a reject batch.
The line works with EPDM, SBR, neoprene, nitrile, and natural rubber blends. The screw and barrel geometry can be specified for either high-friction compounds that need extra shear or softer sponge formulations that require gentler processing.
Depending on profile size and compound density, output usually falls between 150 and 400 kg per hour. Smaller dense profiles run faster by weight; larger sponge profiles occupy more volume even if the mass rate is lower.
A multi-zone cooling bath with adjustable water temperature and a caterpillar or belt haul-off with soft contact pads keeps the profile straight and prevents collapse. The take-off speed is synchronized with extruder output to avoid stretching or buckling.
Yes. The control recipe changes the screw temperature profile and line speed for each material. Sponge compounds need precise temperature staging before the curing oven, while dense rubber can move faster through cooling.
Daily checks focus on screw and barrel wear, gearbox oil temperature, and haul-off belt tension. Weekly cleaning of the die head and calibration sleeves prevents compound build-up. The vacuum pump filters and cooling water strainers should be inspected every 200 operating hours.
Typically, a die and calibration set swap takes 30 to 45 minutes with quick-clamp tooling and preheated heads. The control system stores recipe parameters, so the line returns to stable production after a short purge of the previous compound.
Conclusion
A bulk rubber profile line lives or dies by how steadily material reaches the screw. Hopper design matters less than the metering consistency—a surge bin with a true mass-flow discharge keeps the feed throat full without bridging, so the screw never runs hungry and output stays uniform. When die pressure starts to waver, you'll see it first as thin walls in the profile; that's almost always a feed or temperature imbalance upstream, not a die problem. The fix is to hold melt temperature within a narrow band and let the control loop adjust screw speed against line speed, so you can run faster or slower without the cross-section drifting out of tolerance.
For heavy, thick sections, the cooling trough has to do more than just chill the surface. A multi-zone trough with adjustable spray bars and enough water flow to pull heat from the core prevents the soft rubber from collapsing under its own weight before it sets. Inline cutting then has to match that timing—a rotary knife with servo control and a low-friction anvil slices cleanly without pinching or deforming the still-pliable profile. Finally, data logging ties it all together: recording screw RPM, melt pressure, line speed, and water temperature for every batch means the next run can start from a known-good recipe instead of guesswork.
Contact Us
Contact Person: Chen Zhengwei
Email: [email protected]
Tel/WhatsApp: +86-13963975727
Website: https://www.sfcrubbermachine.com